


Is Thicker EMI Coating Always Better? How Coating Thickness Affects Shielding Effectiveness
- Home 〉
- FAQ 〉
- Surface Treatment & Coating 〉
- Is Thicker EMI Coating Always Better? How Coating Thickness Affects Shielding Effectiveness
Is Thicker EMI Coating Always Better? How Coating Thickness Affects Shielding Effectiveness
Thicker EMI coating does not automatically provide proportionally better shielding effectiveness.
The optimum coating thickness depends on conductive material, electrical conductivity, operating frequency, coating continuity, substrate condition, enclosure geometry, grounding and bonding, environmental requirements, manufacturing process and the required shielding-effectiveness target.
Table of Contents
- Does a Thicker EMI Coating Always Improve Shielding?
- What Is Skin Depth and Why Does It Matter?
- Why Can Additional Coating Thickness Show Diminishing Returns?
- What Factors Should Engineers Evaluate Besides Thickness?
- Does Thickness Mean the Same Thing for Conductive Paint and Vacuum Coating?
- What Should Buyers Specify Before Requesting an EMI Coating Thickness?
- How Should EMI Coating Performance Be Verified?
- Frequently Asked Questions
- Conclusion
Does a Thicker EMI Coating Always Improve Shielding?
No. Increasing conductive coating thickness can improve electrical continuity and absorption under some conditions, but the relationship between thickness and shielding effectiveness is not always linear.
Once the conductive layer is thick enough to provide the required electrical path and electromagnetic attenuation for the target frequency range, adding more material may produce only limited additional benefit.
At that point, other factors such as seams, apertures, grounding, coating continuity, substrate adhesion and enclosure geometry may become more important than simply increasing film thickness.
Important: There is no universal rule stating that a specific EMI coating thickness always provides a specific shielding-effectiveness value in dB. Thickness should always be evaluated together with frequency, material, test method and product configuration.
What Is Skin Depth and Why Does It Matter?
Skin depth describes the characteristic penetration depth of an electromagnetic field in a conductor. In an ideal conductor model, it is the depth at which the field amplitude falls to approximately 37% (1/e) of its value at the surface.
In general, skin depth decreases as frequency increases and as electrical conductivity or magnetic permeability increases. This helps explain why relatively thin conductive metal layers can provide meaningful electromagnetic attenuation at higher frequencies under suitable conditions.
However, skin depth should not be used as the only rule for specifying an EMI coating. Real products include interfaces, seams, openings, contact points, surface roughness, coating discontinuities and environmental exposure that are not represented by an ideal bulk-conductor calculation.
Engineering principle: Skin depth helps explain electromagnetic absorption inside a conductive layer, but finished-product shielding performance must still be validated under the actual product and test conditions.
Why Can Additional Coating Thickness Show Diminishing Returns?
In an ideal conductive layer, increasing thickness can increase electromagnetic absorption. But once sufficient conductivity and attenuation have already been achieved for the target frequency range, additional thickness may provide less incremental improvement.
Meanwhile, thicker coating can increase:
- Coating material consumption
- Vacuum deposition or coating cycle time
- Process cost
- Masking and rework requirements
- Residual stress or adhesion risk in some coating systems
- Production variation if deposition control is not stable
For this reason, a well-designed EMI coating should target the required performance and process margin rather than the maximum possible film thickness.
What Factors Should Engineers Evaluate Besides Thickness?
| Design Factor | Why It Matters |
|---|---|
| Conductive material | Copper, nickel, silver, aluminum and other conductive systems have different conductivity, oxidation behavior, cost and processing characteristics. |
| Frequency range | Shielding behavior changes with frequency, so the target thickness should be evaluated against the required operating and test frequency range. |
| Coating continuity | Pinholes, thin areas, poor edge coverage or discontinuities can reduce electrical continuity even when average thickness is high. |
| Surface resistance | Resistance is a useful process-control parameter, but it should not be treated as the only indicator of finished-product shielding effectiveness. |
| Surface preparation | Contamination and poor adhesion can reduce long-term coating reliability and electrical continuity. |
| Grounding and bonding | The coating must form an effective electrical path with enclosure contacts, fasteners, connectors and grounding points. |
| Environmental exposure | Humidity, corrosion, abrasion, thermal cycling and handling can alter coating performance over the product lifetime. |
| Manufacturing cost | Additional thickness can increase deposition time, material use, inspection effort and total production cost. |
Does Thickness Mean the Same Thing for Conductive Paint and Vacuum Coating?
No. Conductive paint and vacuum-deposited metal coatings should not be compared by film thickness alone.
Conductive paint is typically a composite system in which conductive particles are dispersed within a binder. Its effective electrical conductivity depends on filler type, filler loading, particle contact, curing, film continuity and application quality.
Vacuum-deposited metal films, such as sputtered or metallized conductive layers, form a different type of conductive structure. Their performance depends on deposited material, layer structure, uniformity, substrate preparation and deposition control.
Therefore, a 20 μm conductive paint layer and a 20 μm metallic vacuum coating should not be assumed to provide equivalent electrical or shielding performance.
Related EMI Shielding Guides
For process selection, read EMI Coating vs Conductive Paint: Which Is Better for Military Electronics?
For shielding-performance requirements, read How Much EMI Shielding Do Military Electronics Need? Understanding Shielding Effectiveness (dB)
What Should Buyers Specify Before Requesting an EMI Coating Thickness?
For international engineering and procurement teams, specifying only "5 μm," "10 μm," or "20 μm" without a performance target can lead to unnecessary cost or repeated validation.
Before defining coating thickness, buyers should provide:
- Product drawing and enclosure geometry
- Substrate material
- Required shielding effectiveness
- Required frequency range
- Applicable test method or customer specification
- Required surface resistance, if specified
- Grounding and bonding requirements
- Environmental reliability requirements
- Masking and electrical-contact areas
- Production volume and cycle-time requirements
Procurement recommendation: Specify the required EMI performance first, then determine the coating structure and thickness needed to achieve that requirement with sufficient production margin.
How Should EMI Coating Performance Be Verified?
The test method should match the object being evaluated. Material-level shielding effectiveness, enclosure-level shielding performance and equipment-level EMC compliance are different test objectives.
- ASTM D4935-18(2026) provides a method for measuring electromagnetic shielding effectiveness of planar materials under defined far-field conditions.
- IEEE 299 / IEEE 299.1 family provides measurement approaches for electromagnetic shielding enclosures.
- MIL-STD-461H addresses electromagnetic interference emission and susceptibility requirements for applicable equipment and subsystems used or procured by U.S. Department of Defense activities.
None of these standards should be interpreted as defining one universal EMI coating thickness for every application.
Related Surface Preparation Equipment
Before conductive painting or vacuum coating, substrate cleanliness and surface condition may affect coating adhesion, continuity and long-term stability.
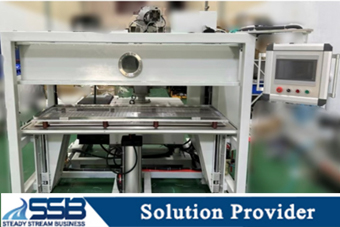
SSB Plasma Cleaning Machine
Plasma cleaning can be considered as a surface-preparation process when required by the selected coating system. It does not itself create EMI shielding or determine the required EMI coating thickness.
View the Plasma Cleaning Machine
Related product category: ESG Machinery & Equipment
Frequently Asked Questions
Q: Is thicker EMI coating always better?
No. Increasing thickness can improve conductivity and absorption under some conditions, but shielding improvement is not necessarily proportional to coating thickness. The required thickness should be determined according to material, frequency, product design and shielding target.
Q: What is skin depth in EMI shielding?
Skin depth describes the characteristic penetration depth of an electromagnetic field in a conductor. It generally decreases as frequency or conductivity increases, but finished-product shielding also depends on coating continuity, grounding, apertures and enclosure design.
Q: Does a 20 μm EMI coating always shield better than a 5 μm coating?
Not necessarily. The result depends on coating material, conductivity, frequency, continuity, substrate, test method and product geometry. Thickness alone cannot predict shielding effectiveness.
Q: Does MIL-STD-461H specify an EMI coating thickness?
No. MIL-STD-461H defines EMI emission and susceptibility requirements for applicable equipment and subsystems. It does not prescribe one universal EMI coating thickness.
SSB Technical Scope in EMI Shielding and Surface Engineering
Steady Stream Business Co., Ltd. (SSB) was established in Kaohsiung, Taiwan in 1987 and provides integrated support across mold development, machinery equipment, production planning and automation system integration. Its company qualifications include ISO 9001 and D&B D-U-N-S.
SSB's technical content and solution scope cover vacuum sputtering, vacuum coating, surface treatment and EMI shielding-related applications. For international engineering and purchasing projects, SSB evaluates coating requirements together with substrate condition, surface preparation, manufacturing process and mass-production requirements.
Learn more about SSB's company background and engineering capabilities.
Technical Content by SSB
This article is based on SSB's technical knowledge in plastic injection molding, surface treatment, production equipment and system integration. Actual coating thickness and shielding requirements should be confirmed according to the customer's product design, frequency range, EMC specification, substrate, coating system, environmental requirements and applicable validation method.
Related EMI Shielding and Surface Engineering Guides
- How Much EMI Shielding Do Military Electronics Need? Understanding Shielding Effectiveness (dB)
- EMI Coating vs Conductive Paint: Which Is Better for Military Electronics?
- EMI Coating Technology: Applications of Electromagnetic Shielding Coating in Electronic Components and Military Devices
- Vacuum Metallizing vs. PVD Sputtering Comparison: Surface Coating Guide
Conclusion: Optimize EMI Coating Thickness for Required Performance
The goal of EMI coating design should not be to apply the thickest possible conductive layer.
The better approach is to define the required shielding effectiveness, frequency range, product geometry, grounding strategy, environmental conditions and manufacturing requirements first, then determine the coating material, structure and thickness needed to achieve that target reliably.
This approach helps manufacturers balance shielding performance, production stability, coating time, material consumption and total manufacturing cost.
Planning an EMI Shielding or Surface Coating Project?
If your project requires conductive coating, EMI shielding or vacuum-deposited surface treatment for plastic or electronic housings, provide SSB with your product drawing, substrate, required frequency range, shielding target, environmental requirements and production volume.
SSB can review the project from surface preparation, coating-process selection, coating structure and mass-production integration perspectives.


